Medical Consumable AI Visual Inspection Equipment
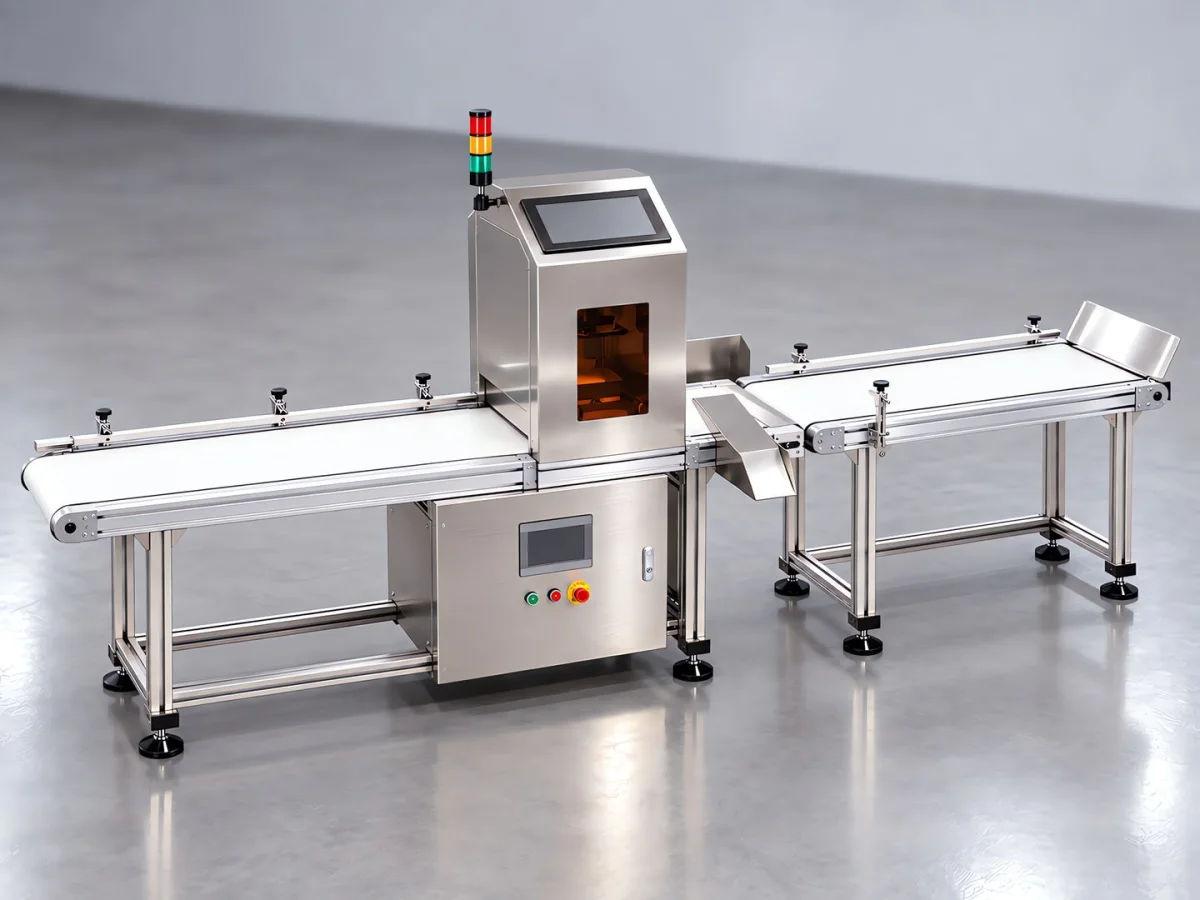
Medical consumables AI visual inspection equipment: for consumables such as medical dressings, adhesive bandages, medical tape, surgical gowns, isolation gowns and medical non-woven fabric, it inspects damage, holes, uneven coating, foreign matter and structural defects, and outputs OK/NG.
Products Overview
Medical consumables place higher demands on cleanliness, traceability, and zero tolerance for defects
Medical consumable AI visual inspection equipment is used for inline inspection of medical dressings, adhesive bandages, medical tape, surgical gowns, isolation gowns and medical non-woven fabric; industrial cameras and light sources identify damage, holes, uneven coating and foreign matter, output OK/NG and interlock with rejection and recording.
Inspection of medical consumables has two requirements that other industries seldom encounter: one is Cleanliness and no contamination, the inspection equipment itself must not become a source of contamination; second, Traceable, and the inspection records of each batch must correspond to the batch or even to individual parts.
At the defect level, the focus for medical dressings and tapes is coating uniformity, damage, and holes; the focus for surgical gowns and isolation gowns is the integrity of the non-woven fabric, seams, and coating; and small items such as adhesive bandages require piece-by-piece inspection.
Because medical consumables are often produced in very large volumes at a low unit price, the cycle time and stability of the inspection solution are usually more important than extreme accuracy.
- Covered categories: medical dressings, adhesive bandages, medical tape, surgical gowns, isolation gowns, medical non-woven fabric
- Typical defects: damage, holes, uneven coating, foreign matter
- Special requirements: cleanliness, traceability
- Solution focus: stable cycle time + batch records
Core Functions
What the Equipment Can Do and How Far It Can Go
Coating Uniformity Check
Inspect whether the adhesive layer and the active-material coating are uniform and free of misses.
Damage and Holes
Transmitted-light imaging is used for thin non-woven fabric and film, so holes are clearly imaged.
Foreign Matter Recognition
Detect mixed-in fibers, particles and other foreign matter.
Piece-by-Piece Inspection
Small items such as adhesive bandages can be inspected and rejected piece by piece.
Batch Records
Records the inspection results and images of each batch, supporting batch traceability.
Hygienic Construction
The equipment structure can be designed for easy cleaning to reduce contamination risk.
inspection Object
Dressings and Tapes
Coating uniformity, dimension, damage and holes
Surgical Gowns and Isolation Gowns
Non-woven fabric integrity, seams, and coating
medical non-woven fabric
Holes, foreign matter and thickness anomalies at the web stage
Small Parts and Consumables
Piece-by-piece appearance and dimensional inspection of small items such as adhesive bandages
inspection defect
| Defect Types | Risk Level | Inspection Focus Points |
|---|---|---|
| Hole / Damage | Critical | Affects protection and bacteria barrier performance; transmitted-light imaging is the most direct method |
| Uneven coating / missing coating | Critical | Affects functional layer performance |
| Foreign Matter / Impurity | Critical | High cleanliness requirements; fiber texture must be carefully distinguished |
| Uneven edge / out-of-tolerance dimension | Moderate | Affects downstream processing and use |
| Stain / Color Difference | Moderate | Appearance and acceptance related |
| Seam Defect | Moderate | Stitching quality of surgical gowns and isolation gowns |
| Fold and indentation anomaly | Slight | Affects packaging and user experience |
Working Principles
- 01 Roll unwinding or small-part loading
- 02 Tension and position control
- 03 Triggered Imaging
- 04 Transmitted-light hole inspection
- 05 Coating and surface inspection
- 06 Foreign Matter Recognition
- 07 Result Composition OK / NG
- 08 NG Marking or Rejection
- 09 Batch record archiving
Relationship Between Imaging and Judgement
What makes medical consumable inspection special is The equipment itself is part of the quality system: the structure must be easy to clean, materials must meet site requirements and inspection records must be traceable. These non-algorithm factors often determine success or failure in actual projects.
Vision System
How Cameras, Lenses, Light Sources and Controllers Are Configured
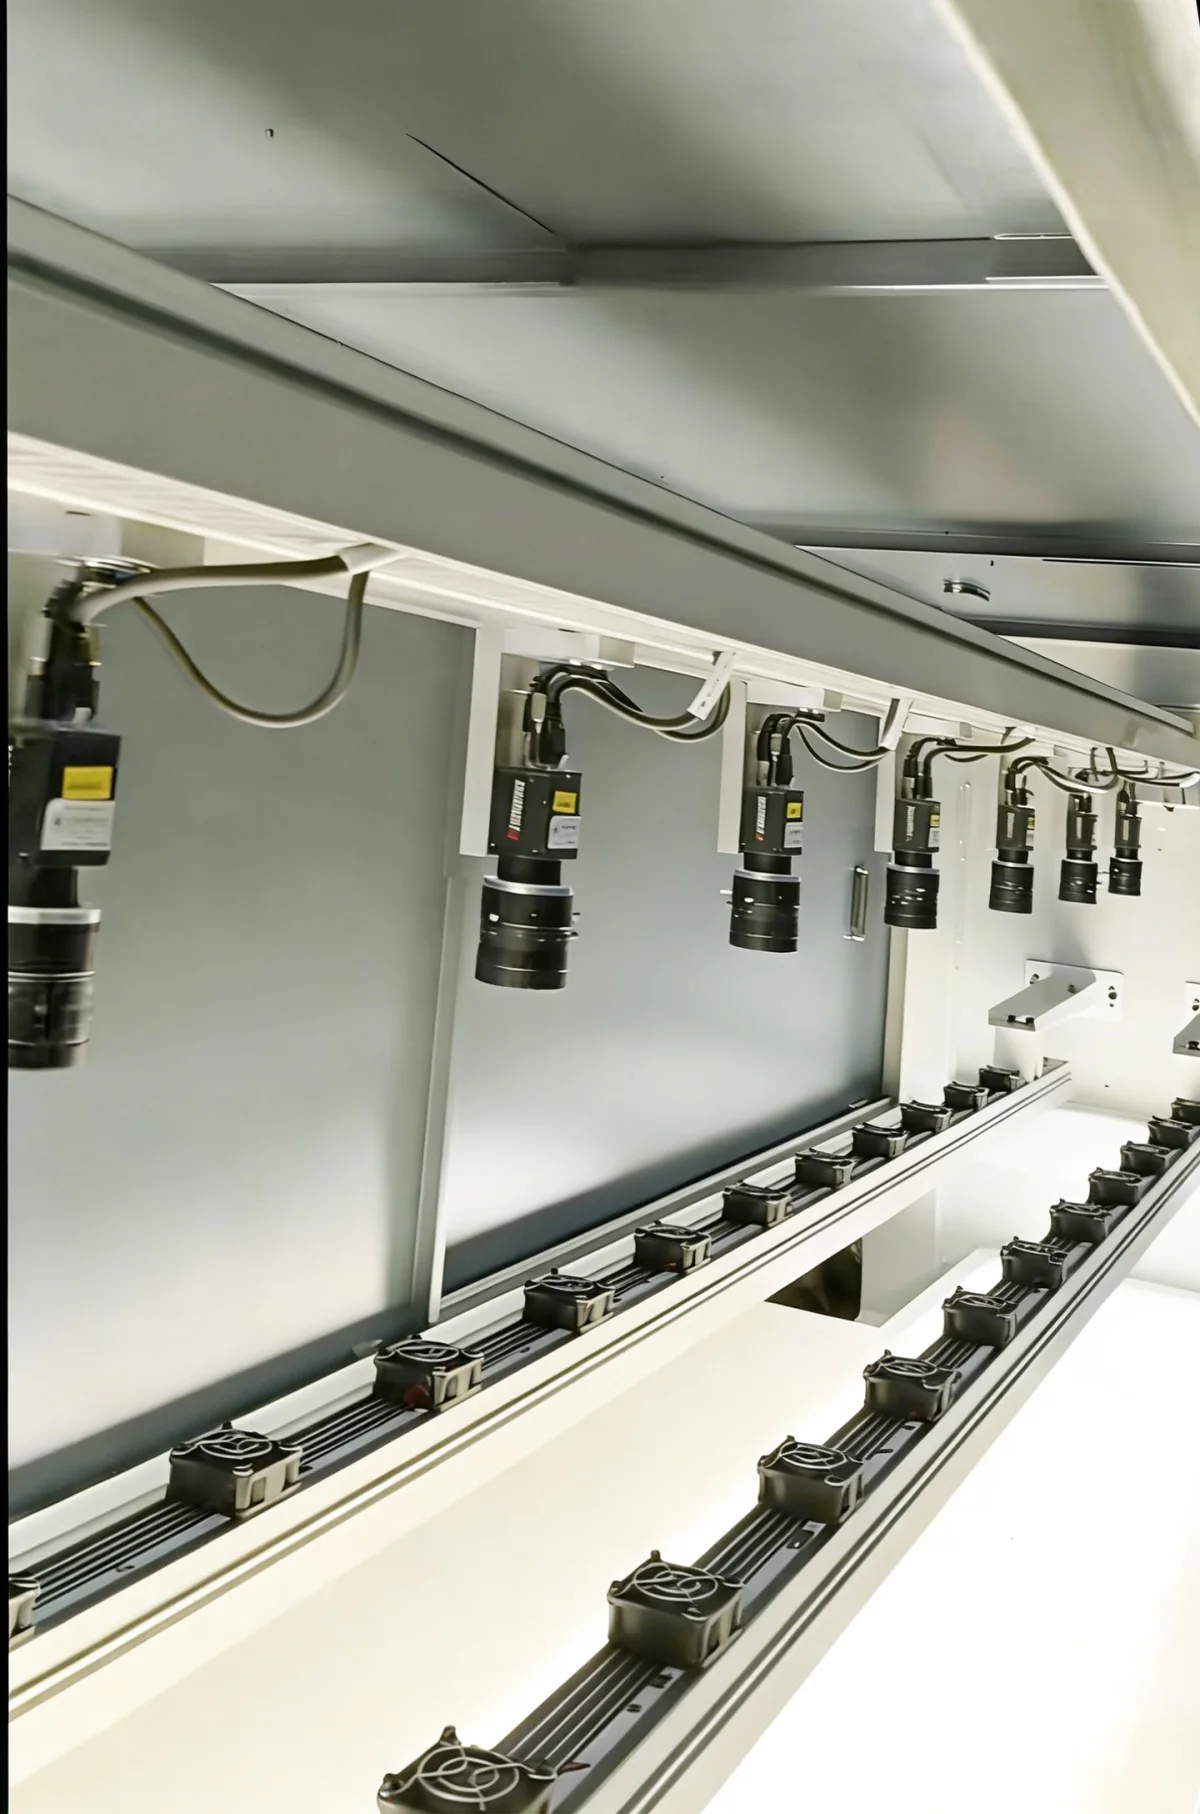
industrial camera
Select area-scan or line-scan by field of view and minimum defect size; continuous web materials usually use line-scan cameras
- Area-scan camera: fixed-shot, single-piece and intermittent feed applications
- Line-scan camera: for continuous material travel, wide areas, and even-interval imaging
- Pixel equivalent is derived backwards from "minimum resolvable defect ÷ desired pixel count", rather than fixing the camera first
lens
Determines field of view, distortion, and depth of field; precision measurement requires telecentric lenses
- Standard industrial lens: low cost, suitable for appearance inspection
- Low-distortion lens: for large-format applications where the edges must also be judged
- Telecentric lens: suitable for hole diameter, contour and dimensional measurement
- Depth of field must match material waviness and fixture repeat positioning accuracy
Light Source and Illumination
Whether defects in flexible materials can be captured depends largely on the lighting
- Diffuse light: uniform illumination, suitable for color difference and stain applications
- Low-angle light: highlights scratches, indentations, wrinkles and other surface relief
- Backlight/transmitted light: highlights holes, damage and short shot
- Coaxial light / stripe light: suppresses reflection, suitable for coated or highly reflective surfaces
Controllers and Industrial PCs
The platform for running algorithms, outputting results and interlocking with the production line
- An industrial computer or vision controller runs the algorithms
- A light source controller handles brightness adjustment and strobe synchronization
- Interacts with the PLC to complete interlocking, alarming, and rejection
AI algorithm
Choose the Algorithm by Defect Form, Not by Complexity
Template Matching and Positioning
Locate first, then judge. Every defect judgment is built on a stable coordinate system.
- Shape matching / gray-scale matching: good stability, suitable for fixed stations
- Align first, then split the regions, to avoid false calls caused by position drift
Blob and Morphological Analysis
Suited to defects such as stains, holes and foreign matter that show a clear grayscale/color difference from the background
- Threshold segmentation → connected component statistics → judgement by area / aspect ratio / circularity
- High requirements on illumination stability; the light source must work with the fixture
Edge and Contour Measurement
Suitable for dimension, contour, hole position and spacing judgements
- Sub-pixel edge extraction to obtain a contour point set
- Fit lines/circles/arcs and calculate length, diameter, angle and position tolerance
Deep Learning (Classification / Detection / Segmentation)
Suited to defects such as scratches, wrinkles and skipped stitches, whose shapes vary and are hard to describe with rules
- When defect forms are irregular, it is difficult for rule-based algorithms to enumerate them all
- Requires OK / NG sample training; sample quantity and coverage determine the upper limit
- Enables pixel-level segmentation and outputs defect length, width, area and position
Automatic Alarm and rejection
How inspection results act on the production line
Inspection results are not only shown on a screen. Workpieces judged NG need to be Mark the position and interlock rejection or sorting, and archives the image and judgement result for that part for later traceability and re-judgement.
The alarm method is set according to site practice: audible and visual alarm, on-screen pop-up, PLC set bit, or all three at once. Critical defects and general defects can use different handling strategies — the former stops the machine and alarms, the latter is only marked.
- 01 image acquisition
- 02 Positioning and region segmentation
- 03 Defect Judgement
- 04 Combine results into a single OK / NG per piece
- 05 Result sent to PLC
- 06 NG Rejection / Sorting
- 07 Image and data archiving
data traceability
Records, Queries and Quality Closed Loop
Per-Piece Records
The judgment result, defect type, defect position and timestamp of every part are written to the database
- Supports retrieval by time, batch and defect type
- NG image retention for re-judgement
Batch and Recipe
Different products use different recipes, called up at changeover to reduce manual parameter tuning
- Recipes store the inspection region, thresholds and algorithm parameters
Production Line Data Integration
Exchange inspection data with the MES / host system
- Output pass rate, defect distribution and other statistics
- The interface method depends on the site system
equipment configuration
Optional Configuration Items and Selection Logic
| Configuration Item | Description |
|---|---|
| Applicable Categories | Medical dressings / adhesive bandages / medical tape / surgical gowns / isolation gowns / medical non-woven fabric |
| Inspection Method | Transmitted light + reflected light combined imaging + AI algorithm |
| Structural Requirements | Can be customized to site cleanliness and hygiene requirements |
| Recording Method | Recorded by batch (content and interval customizable) |
| Inspection Speed | To be added |
| inspection accuracy | To be added |
| communication method | I/O · TCP · RS485 · Modbus · S7 · Profinet |
| Enclosure and Material | To Be Confirmed on Site |
Application Industry
Which Industry This Equipment Is Usually Installed In
Applicable Materials
Detectable Material Types
Common Question
How are holes in medical non-woven fabric detected?
Does the equipment meet cleanroom requirements?
Can Inspection Records Be Traced?
Can small items such as adhesive bandages be inspected piece by piece?
How Is Uneven Coating Judged?
What Information Do You Need to Provide?
Submit sample testing
Key defects on medical consumables require zero escapes and depend even more on physical validation. Please provide NG samples containing defects and your cleanliness requirements, and we will evaluate them together.
Submitted successfully
We have received your sample testing request. A solution engineer will contact you within 1 business day via contact you.
Need to assess imaging conditions, defect criteria and cycle time item by item? Go to the Full Requirement Assessment →
Send Us Your Workpiece and We Will Show You the Measured Results
Equipment configuration varies with the inspection object, field of view and cycle time. Provide OK and NG samples and we will run actual imaging and judgement tests and recommend the corresponding model and configuration.