Connector Presence/Absence Inspection
Judges whether connectors are installed, fully inserted and of the correct model, covering common anomalies such as missing part, not fully inserted and wrong model.
inspection Overview
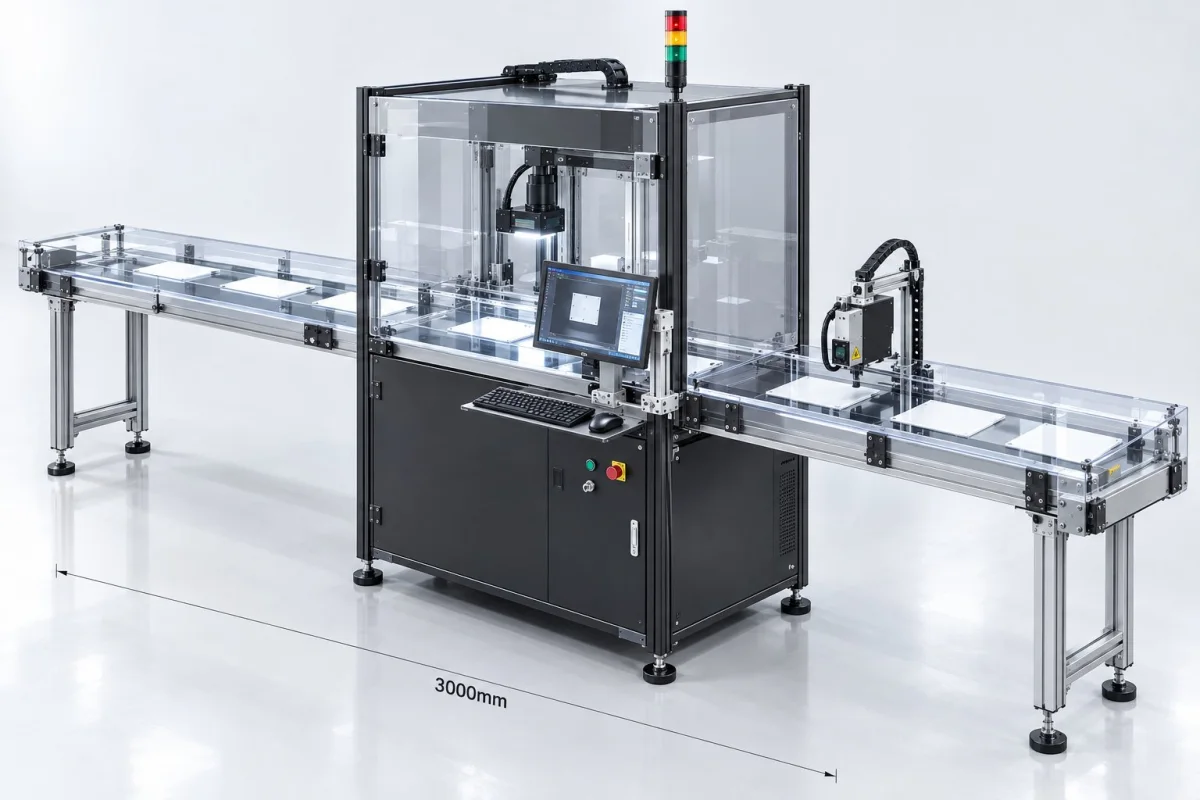
Connector presence/absence inspection: determine whether the connector is installed, whether it is fully plugged in and whether the model is correct, covering common anomalies such as missing parts, not fully seated and wrong model. The judgement usually does not check details such as threads or dimensions, but rather determines Whether the visual feature at that position exists and matches expectations, output OK / NG and interlock with the production line.
Judges whether the connector is installed, fully seated and of the correct model, covering common anomalies such as missing part, not fully inserted and wrong model.
The feasibility of "connector presence/absence inspection" depends on Whether the visual features of the object are stable and distinguishable, as well as the on-site optical and tooling conditions. Each item is expanded below in the order commonly used in inspection engineering.
Object Characteristics
How the object appears in the image
- Many forms; different positions in the same series look similar
- Fully seated or not often comes down to a very small gap
- Plastic housings come in many colors and may have clip locking structures
- Mounting positions are often deep or blocked by surrounding parts
inspection Challenges
Where Problems Really Occur on Site
- Different pin counts in the same series (such as 4P and 6P) look alike; count the positions or measure the width
- The difference between "plugged in" and "fully seated" is small
- Deep cavities are difficult to illuminate
- Harness swing causes an unstable viewing angle
Vision Judgement method
How acceptance criteria are set and why
Presence/absence judgement checks whether the connector housing is in place; the seated judgement checks Mating gap or Clip locking state; model judgement relies on Width, position count or marking features.
The three have different acceptance criteria; implement them in the order of what matters most on site rather than pursuing full coverage at once.
Applicable algorithm
Choose by the Form of the Acceptance Criteria, Not by Complexity
Presence judgement
Determine whether the connector housing is present
Geometric Measurement
Measure the mating gap or width to judge whether the connector is fully seated / whether the model is correct
Classification
Distinguish models by features in multi-model mixed-line production
Optical Precautions
Imaging conditions set the upper limit of feasibility
- For deep cavities, light guides or coaxial illumination are recommended so that housing features stay visible
- The mating face usually requires a side view to observe the gap
- When multiple models are mixed on the same line, consistent illumination matters more than absolute brightness
OK / NG Output
How results are judged and passed to the production line
| Inspection Status | judgement | Interlocking Action |
|---|---|---|
| Connector present, fully plugged in, correct model | OK | release |
| No connector detected | NG | Block as missing part |
| Not fully mated or wrong model | NG | Handled as assembly defect / wrong material |
Applicable Industry
This type of inspection is common in the following industries
Common Question
The most common questions about this object
Can 4P and 6P connectors be distinguished?
Yes, mainly from width or position-count features. A difference in position count appears in the image as the number of contact points or the housing width, and as long as they image clearly they can be distinguished reliably. If the two have the same width and differ only in internal structure, a dedicated angle is required.
How Do I Judge Whether It Is Fully Mated?
It usually comes down to whether the gap between the mating faces has closed, or whether the locking marks on the housing are aligned. This requires a viewing angle that can see the mating faces; a top-down view is usually not enough.
What are the acceptance criteria for this object?
Presence/absence judgement checks whether the connector housing is in place; seating judgement checks the insertion gap or clip locking state; model judgement relies on width, pin count or marking features.
What are the illumination requirements for this type of object?
For deep cavity positions we recommend light-guide or coaxial illumination to keep housing features visible. Mating faces usually need a side view to observe the gap
What Are the Inspection Accuracy and Minimum Detectable Size?
It depends on the combination of field of view and camera resolution, and is affected by the lens, illumination and algorithm. To be added — the configuration must be derived from your minimum defect size, subject to the results of a measured sample trial.
How Do We Verify That Our Product Can Be Detected?
Please provide a fully inserted part, a not fully inserted part and samples of different connector models; our engineers will evaluate the distinguishing features.
Submit sample testing
Please provide a fully inserted part, a not fully inserted part and samples of different connector models; our engineers will evaluate the distinguishing features.
Submitted successfully
We have received your sample testing request. A solution engineer will contact you within 1 business day via contact you.
Need to assess imaging conditions, defect criteria and cycle time item by item? Go to the Full Requirement Assessment →
Send Us Your Workpiece and We Will Show You the Measured Results
Provide several OK and NG samples, and the solution engineer will run actual imaging and judgement tests on the equipment, then give inspection configuration recommendations that can be implemented, rather than just reading a specification table.