Rubber Seals
For rubber seal production, providing appearance defect, dimension and assembly inspection solutions, applicable to products such as O-rings, oil seals and gaskets.
Industry Production characteristics
How This Industry Produces Determines How Inspection Should Be Done
The visual inspection of rubber seals revolves around two things: first, making the most common defects in this industry image clearly and consistently; second, connecting the judgement result reliably into the production line. Common implementation constraints in this industry are "black rubber absorbs light, making surface details hard to reveal"; "flexible parts do not hold a fixed shape during conveying". Whether detection can be stable depends on material optical properties, minimum defect size, and cycle time, and is subject to the results of a measured sample trial.
Rubber seals are characterized by Flexible, dark colored, textured surface, and all three pose challenges for visual inspection: flexibility means the shape is not fixed, dark color means low contrast, and texture is easily confused with defects.
Inspection in this industry typically requires Dedicated optical design — conventional diffuse illumination often cannot reveal defects on the surface of rubber parts.
Industry Inspection issues
Where problems actually occur on site
- Short shot, missing adhesive
- Flash, burr
- Bubbles, inclusions
- Out-of-tolerance dimension (inner/outer diameter, cross-section)
- Low hardness leads to deformation (indirect indication)
Typical Inspection Objects
The Most Common Inspection Objects in This Industry
Typical Inspection Task
The judgments to be made on these objects
- Appearance defect identification
- Inner and outer diameter dimensional measurement
- Flash and short shot inspection
- Count check
- Assembly State Confirmation
Vision Inspection Challenges
Implementation constraints specific to this industry
- Black rubber absorbs light, so surface details are hard to reveal
- Flexible parts do not hold a fixed shape during transfer
- Texture and defects are easily confused
- High volume, high speed required
Choosing the right algorithm
Choose by Acceptance Criteria Form, Not by How Advanced It Is
Anomaly Detection
Surface defect identification
Geometric Measurement
Inner/outer diameter and cross-section dimension measurement
Target Segmentation + Counting
Count check
acquisition and light source
Optical conditions set the upper limit of feasibility
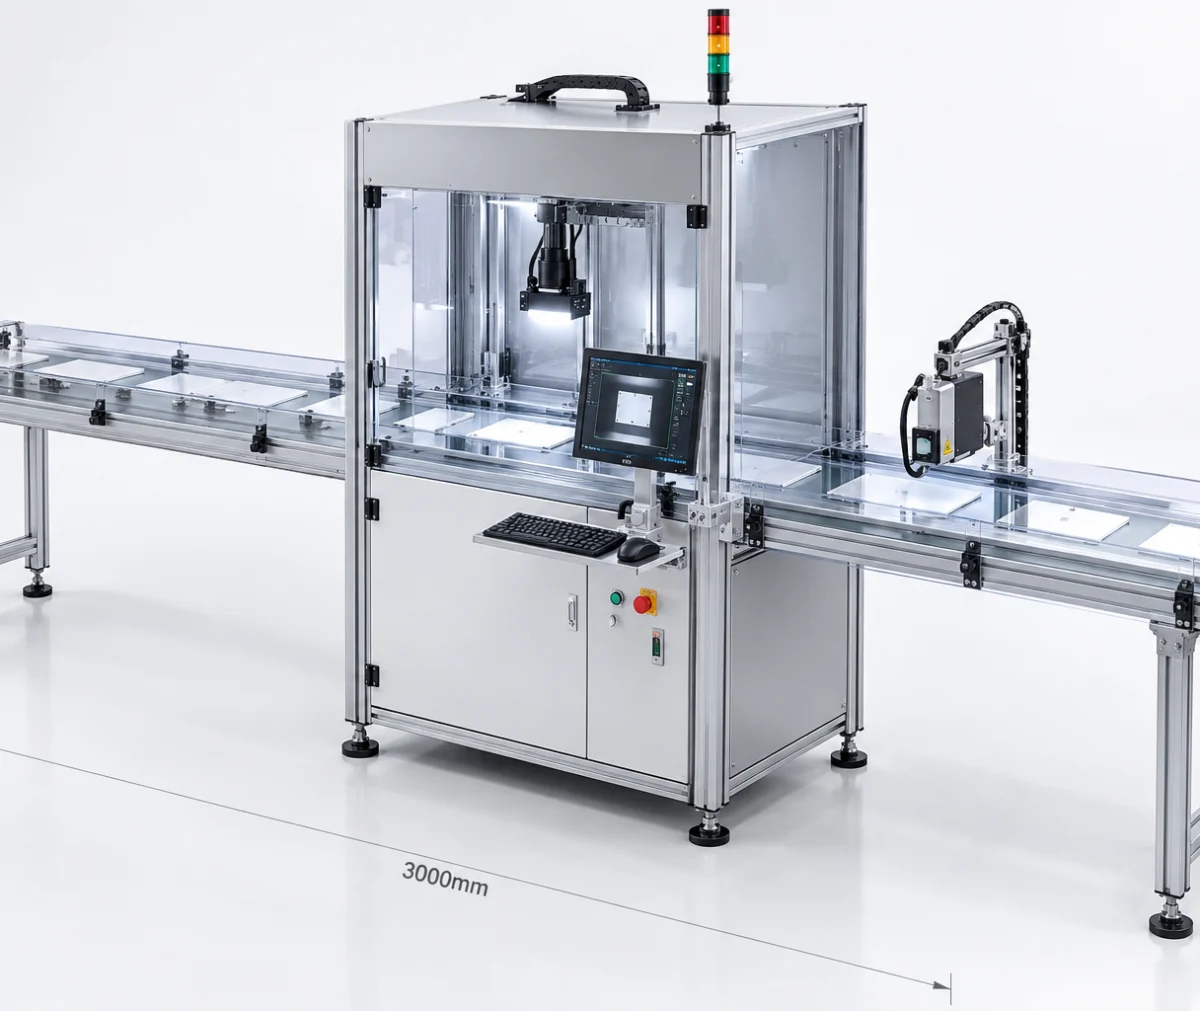
- Backlighting can be used for contour and dimensional measurement and is the most stable solution
- For surface defects, low-angle grazing light is recommended to highlight relief
- For dark rubber parts, increase illuminance or use illumination at a specific wavelength
OK / NG Judgement
How results are judged and used
| Inspection Status | judgement | Interlocking Action |
|---|---|---|
| Appearance and dimension pass | OK | release |
| Short shot / flash / bubble present | NG | rejection |
| out-of-tolerance dimension | NG | Reject and prompt a mold check |
PLC and Automation Interlocking
How results connect to the production line
Clustered dimensional defects usually point to mold wear; outputting trend information for preventive maintenance is recommended.
When interlocking with the sorting mechanism, note the reliability of rejecting small parts.
Applicable equipment
Common configuration forms for this type of inspection
Related Solutions
View the corresponding solution by inspection task
Common Question
The Questions Most Often Asked in This Industry
Can appearance defects on black O-rings be detected?
This is the difficult part. Feasible directions include low-angle grazing light to highlight surface relief and specific wavelengths to enhance material differences. The feasibility and the detectable defect size must be validated with actual samples.
How Are Dimensions Measured on Flexible Parts with No Fixed Shape?
Measurement is usually done after tooling holds the product in a stable form (for example placed in a locating slot or flattened). If the product's shape fluctuates widely in its free state, direct measurement produces a large number of false calls.
For visual inspection in this industry, what needs to be solved first?
The implementation constraints commonly seen in this industry center on: "black rubber absorbs light, making surface detail hard to reveal"; "flexible parts do not hold their form during conveying"; "texture and defects are easily confused". These constraints affect both the imaging solution and the cycle-time design. Normally a sample trial is needed to validate before the configuration is finalized.
How does the inspection result interlock with the production line?
A cluster of dimensional defects usually points to mold wear, so output trend information for preventive maintenance. When interlocking with a sorting mechanism, pay attention to the reliability of small-part rejection.
What Equipment Configuration Does This Type of Inspection Generally Require?
Common forms include: "high-speed sorting inspection machine", "backlit dimensional inspection station", and "appearance inspection station". The specific machine model and quantity depend on the inspection area, minimum defect size, and line cycle time, and must be confirmed according to site conditions.
Which process steps in this industry benefit most from a visual inspection station?
The most common is: "appearance defect recognition"; "inner and outer diameter dimensional measurement"; "flash and short shot check". Which process steps to actually instrument depends on the cost of defects escaping downstream and of rework — the later a defect is found, the higher the cost.
How do we judge whether our product is suitable for visual inspection?
Please provide conforming parts and parts with known defects (short shot, flash, bubbles), and state the dimensional tolerance requirements and daily output. In general, as long as the acceptance criteria can be stated clearly, defects image clearly and consistently, and the cycle time matches the field of view, the project is feasible.
What inspection accuracy can be achieved?
Accuracy is not a fixed value that holds regardless of conditions. To be added — the minimum detectable size depends on the combination of field of view and camera resolution, and is also affected by illumination, lens and algorithm; the configuration must be derived from your minimum defect size and validated by measurement.
Submit sample testing
Please provide good parts and known defect parts (short shot, flash, bubbles), and state the dimensional tolerance requirements and daily output.
Submitted successfully
We have received your sample testing request. A solution engineer will contact you within 1 business day via contact you.
Need to assess imaging conditions, defect criteria and cycle time item by item? Go to the Full Requirement Assessment →
Inspection Configuration Based on Your Industry's Products and Cycle Time
Send us photos of the workpiece, the inspection requirement (what to inspect, and the tolerance for escapes and false calls), and the line cycle time, and our solution engineers will recommend the inspection method, optical solution, and interlocking configuration for that industry.